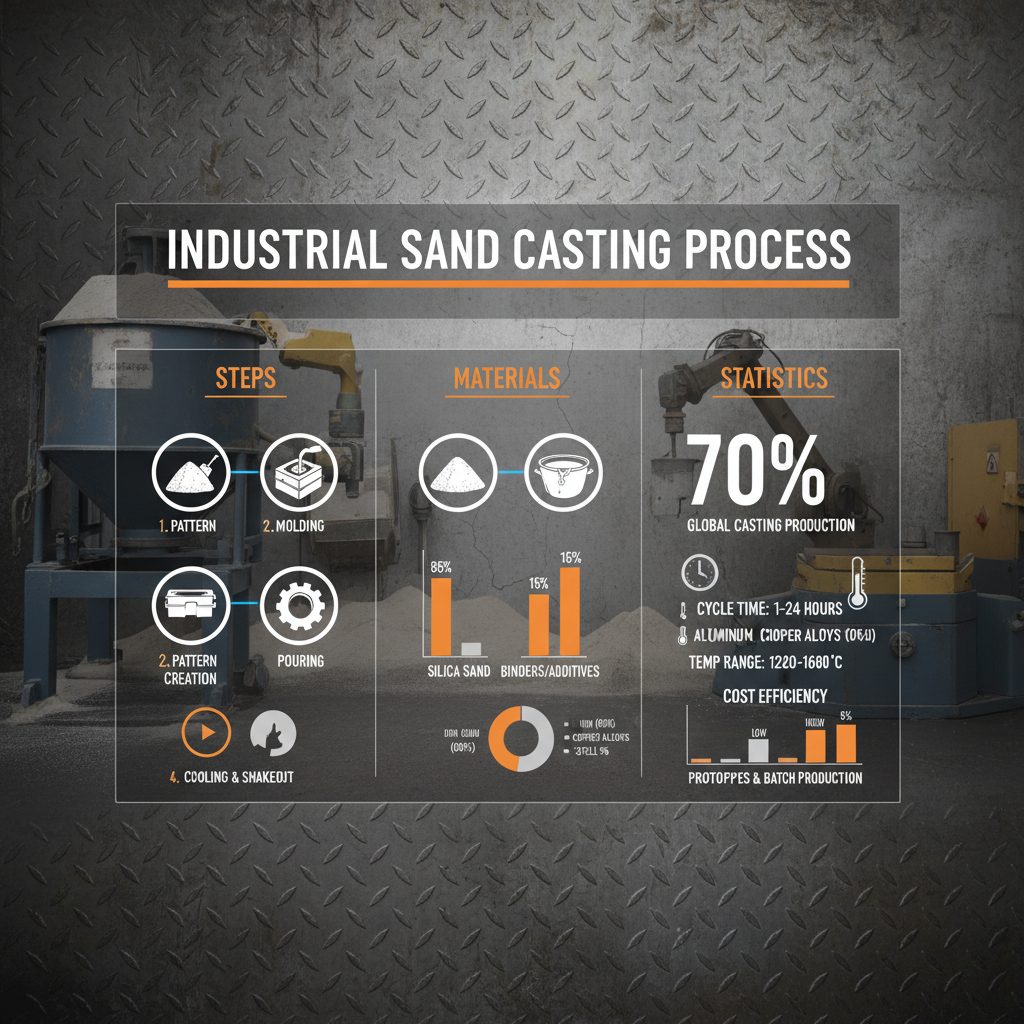
The transition from prototyping to sand casting mass production often reveals a critical bottleneck: the inconsistency of traditional silica sand. When production volumes scale, small variations in mold stability and thermal expansion lead to exponential increases in scrap rates and machining costs.
Modern foundries are increasingly moving away from natural sands toward engineered ceramic media to stabilize these variables. By controlling the mineralogical composition and grain geometry, manufacturers can achieve tighter tolerances and higher surface finishes, which are essential for high-throughput industrial environments.
This analysis explores the technical shifts enabling high-volume casting stability, focusing on how advanced ceramic sands reduce binder consumption and improve reclamation rates in diverse alloy applications.


Traditionally, silica sand dominated the industry due to availability, but its tendency for phase transformation at high temperatures often creates internal stresses in the casting. As the industry pushes for sand casting mass production, the demand for "Sintered Ceramic Sand" has surged as a viable substitute for fused ceramic sand and zircon sand.
These engineered materials, characterized by a Mullite and Corundum composition (Al₂O₃≥53%), provide a neutral PH value and exceptional refractoriness (≥1800℃), ensuring they remain chemically inert when in contact with molten steel, iron, or non-ferrous alloys.
In mass production, the speed at which a mold is filled determines the cycle time. Traditional angular sands create friction, requiring higher pressure or more binder to ensure the mold is completely filled. Engineered ceramic sands solve this through a controlled spherical shape with an angular coefficient ≤1.1.
This spherical geometry reduces the specific surface area of the grains. When the surface area is minimized, the amount of binder—whether furan, sodium silicate, or phenolic urethanes—required to reach the same mold strength is significantly lowered. This not only reduces raw material costs but also enhances the venting ability of the mold.
Chemically, the presence of Al₂O₃ and SiO₂ ensures that the material maintains structural integrity. The low L.O.I. (
One of the primary causes of casting defects in high-volume runs is thermal expansion. When sand expands unevenly during the pour, it can cause "scabs" or dimensional warping. Ceramic sand is engineered with a low thermal expansion rate (4.5-6.5x10⁻⁶/k between RT and 1200℃).
The correlation between low thermal expansion and casting yield is direct: reduced internal mold stress leads to fewer cracks, better dimensional repeatability, and a significant increase in total output per mold.
This stability is further bolstered by high refractoriness. Because the mineralogical composition is dominated by corundum and mullite, the sand does not soften or fuse at the temperatures required for stainless steel or ductile iron casting, maintaining the precise geometry of the cavity throughout the cooling process.
The relationship between grain shape and binder consumption is a critical cost driver in mass production. Spherical grains pack more efficiently, leaving smaller and more uniform interstitial spaces. This means a thinner layer of binder is required to create a strong bridge between particles.
Furthermore, the increased permeability associated with spherical packing allows gases to escape more freely during the pour. This reduces the occurrence of gas porosity in the final casting, which is often the most common reason for part rejection in large-scale foundries.
Engineered ceramic sands are not limited to a single metal. Their neutral PH and chemical stability make them suitable for aluminum, gray and ductile iron, steel, copper, and magnesium. In a typical industrial setting, a foundry can standardize its sand base and simply adjust the binder system—such as switching from furan to shell resins—depending on the specific alloy requirements.
The adaptability of this material is further enhanced by customizable particle size distributions. From 45μm to 2000μm, the grain size can be tailored to match the wall thickness of the casting, ensuring that the surface finish is optimized for the specific part geometry while maintaining the necessary structural strength of the mold.
In sand casting mass production, sand is a recurring cost. The ability to reclaim and reuse sand is paramount for both economic viability and environmental compliance. Traditional silica sand often breaks down into "fines" during reclamation, leading to high waste volumes and pollution.
Sintered ceramic sand possesses higher particle strength, which significantly lowers the breakage rate during mechanical reclamation. This results in a higher reclamation rate and reduces the amount of fresh sand that must be added to the system, effectively lowering the cost per casting.
From a sustainability perspective, the reduced binder usage and lower waste output align with green manufacturing standards. This is particularly relevant for foundries operating under strict ISO14001 environmental certifications, where waste reduction is a key performance indicator.
Selecting the right media requires a balance between initial material cost and total process cost. While ceramic sand has a higher unit price than silica, the "total cost of ownership" is often lower due to reduced scrap rates and lower binder consumption.
Foundries should evaluate their specific pain points—whether it be dimensional inaccuracy, high gas porosity, or excessive waste—to determine the ideal grain size and composition. For instance, finer grains are preferred for intricate aluminum parts, while coarser grains are better for heavy steel castings.
The following framework compares typical performance metrics across common industrial sand types used in high-volume environments.
| Evaluation Factor | Silica Sand | Zircon Sand | Sintered Ceramic Sand | Impact on Yield |
|---|---|---|---|---|
| Thermal Expansion | High | Very Low | Low | Critical for Dimensions |
| Flowability | Moderate | Low (Heavy) | High (Spherical) | Cycle Time Speed |
| Binder Demand | Baseline | Moderate | Low | Direct Material Cost |
| Refractoriness | Moderate | Very High | High (≥1800℃) | Prevents Fusion |
| Reclamation Rate | Moderate | High | Very High | Waste Reduction |
| Surface Finish | Standard | Excellent | Good to Excellent | Post-Processing Cost |
Sintered ceramic sand offers superior thermal stability and a spherical geometry that silica sand lacks. This results in lower thermal expansion, reducing casting defects like cracks and warping. Additionally, its high flowability allows for faster mold filling and reduced binder consumption, which are critical for maintaining high throughput and reducing costs in mass production environments.
The spherical shape reduces the total surface area of the sand grains compared to angular grains. Since binders coat the surface of the sand to create bonds, a lower surface area means less binder is needed to achieve the same structural mold strength. This efficiency leads to direct cost savings in raw materials and improves the permeability of the mold.
Yes, it is engineered to be compatible with most industrial binder systems, including phenolic urethanes, furan, sodium silicate, bentonite clays, shell resins, and alkyd oils. Its neutral PH value prevents adverse chemical reactions with these binders, ensuring consistent mold strength across various casting processes.
With refractoriness ≥1800℃, this sand remains stable even when pouring high-temperature alloys like stainless steel or cast steel. This prevents the sand from sintering or fusing to the metal surface, which eliminates "burn-in" defects and ensures that the casting surface remains smooth and true to the mold design.
Sustainability is improved through two main paths: reduced waste and reduced chemical use. The high particle strength of sintered ceramic sand ensures a very low breakage rate during reclamation, meaning less sand ends up in landfills. Simultaneously, the reduction in binder usage lowers the emission of volatile organic compounds (VOCs) during the casting process.
While standard sizes work for many, customization is critical for precision parts. Finer particles are essential for achieving high-quality surface finishes on thin-walled components, whereas coarser particles provide better venting and strength for larger, heavier castings. Tailoring the mesh size allows foundries to optimize the balance between surface quality and mold permeability.
Achieving stability in sand casting mass production requires a move from opportunistic material use to engineered precision. By adopting sintered ceramic sands with controlled spherical geometry and high Al₂O₃ content, foundries can simultaneously lower their scrap rates, reduce binder costs, and improve their environmental footprint.
As the industry moves toward tighter tolerances and more sustainable practices, the integration of high-performance ceramic media will likely become the standard for any operation seeking to scale production without sacrificing quality or increasing waste.